Mushroom Leather: A Bio Material for Limited Custom Carrier Drops
Yes, but plan it as a capsule, not a catalogue line. Mushroom leather is grown from mycelium on an agricultural substrate over roughly two to four weeks, then pressed and finished into a 1.0-2.0 mm sheet. It is supple, takes emboss and laser marking well, and suits MOQ 500 unit limited drops where a 10-15 percent shade and texture variation between panels is presented as proof of origin rather than as defect.
Executive summary. Mycelium is the most distinctive bio material available to a carrier brand and the least forgiving one to plan around. Treat it as a limited-drop material: reserve the grow batch first, design the pattern for panel variation, and build the marketing around the growth cycle rather than around performance claims. Where the material is weak, compensate in the pattern, moving base, gusset and interior load paths onto a proven woven so the grown panel never carries structural work. Commercial terms hold at MOQ 500 pieces per colourway, sampling in 6-10 working days once the grade and finish are fixed, bulk in 35-50 days after approval, and inspection at AQL 2.5 with an extended defect list that names texture voids, density variation and edge friability. Budget a higher sampling contingency than you would for a synthetic, because grown sheets vary between batches and the first lot is rarely the last word. Documentation: OEKO-TEX on the finishing chemistry, REACH and Prop 65 declarations, and a written statement of the substrate and binder system.
A custom pet bag programme is usually a size ladder rather than a single style, and the ladder is what determines how many colourways you can afford.
What Mycelium Leather Is and How a Sheet Is Actually Grown
Mushroom leather is not made from mushrooms in the way most people assume. It is grown from mycelium, the root network of a fungus, which is fed on an agricultural substrate such as sawdust, hemp hurd or crop residue. Over a period of roughly two to four weeks the mycelium colonises the substrate and binds it into a dense mat. That mat is then dried, pressed, and finished into a sheet with a leather-like hand.
The growth stage is the part that matters to a designer, because it is where the material's character is decided. Substrate particle size sets the surface texture: a coarse substrate gives a visibly fibrous face, a fine one gives something closer to a milled nappa. Growth time sets density. Pressing sets thickness and stiffness. Every one of those is a variable your supplier controls, and every one of them should appear on your specification.
What arrives for cutting is typically a 1.0 to 2.0 mm sheet, sometimes backed with a woven textile for stability, sometimes supplied unbacked and laminated later. Weight varies widely with density, but a finished carrier panel will usually land in the same band as a mid-weight PU.
The result is a material with an unusual combination of properties: soft and slightly springy in the hand, warm to the touch, breathable in a way coated synthetics are not, and visibly irregular. That irregularity is either the entire reason you are specifying it or the reason you should not.
For a pet carrier brand, mycelium's appeal is narrow but strong. It photographs beautifully, it generates press interest out of proportion to its volume, and it lets a small brand appear at the front of a material conversation that much larger competitors are still watching from the sidelines. It also tends to earn editorial coverage and retailer curiosity that a conventional synthetic simply will not, which for a young label can be worth more than the material's physical properties. The cost of that position is a planning discipline most first-time bio-material buyers have not yet built, and this article is largely about building it.
Reading a Mycelium Spec Sheet Without Being Misled
Suppliers in this category are young, and their data sheets vary enormously in quality. Some publish full mechanical test data; others publish a lookbook. Ask for the numbers, and be specific about which ones you need before you commit to a sampling round.
| Parameter | Typical range | Why it matters |
|---|---|---|
| Thickness | 1.0 - 2.0 mm | Thicker sheets press better but resist tight folds |
| Density | 0.35 - 0.60 g/cm³ | Low density feels soft but abrades quickly |
| Tensile strength | 4 - 12 MPa | Below 6 MPa the panel needs a woven reinforcement |
| Elongation at break | 15 - 40 percent | High elongation means the panel will creep under load |
| Water absorption | Moderate unless finished | Drives the need for a liner and a top-coat |
| Tear strength | 15 - 40 N | The property that decides whether stitch lines hold |
| Sheet size | Often smaller than synthetic rolls | Sets nesting yield and panel size limits |
Tear strength is the number I would insist on above all others. A material can have an acceptable tensile figure and still fail catastrophically at a stitch line, because tear resistance is what determines whether a seam holds when the panel is loaded. If a supplier will not publish it, treat that as information about the supplier.
Sheet size deserves a specific question. Grown sheets are frequently produced in smaller formats than synthetic rolls, which constrains the largest continuous panel you can cut. If your design depends on a single uninterrupted front face, confirm the available sheet dimension before you finalise the pattern, not after.
Finally, ask what the finish is. An unfinished mycelium sheet will absorb water and stain; a finished one will resist both but may contain a synthetic top-coat that changes the sustainability story. Both are legitimate; you simply need to know which one you are buying and describe it accurately to your customer. Ask for the finish composition in writing as part of the quotation, because it is the single most common source of a claim problem further down the line.
Consistency and Yield: The Honest Constraints of a Grown Material
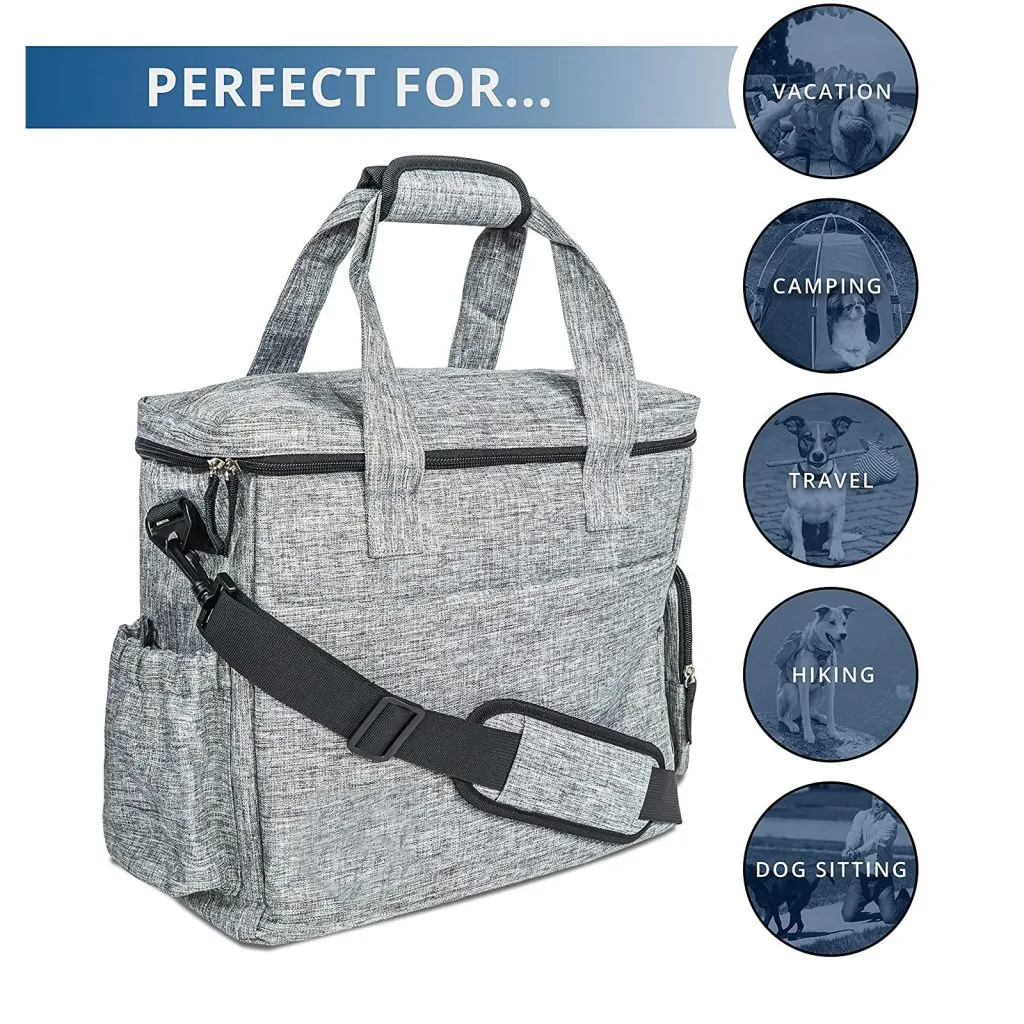
Every bio-material has a variability story, and mycelium's is the most pronounced. Two sheets from the same grow batch can differ in density, in surface texture, and in shade. Two batches grown a month apart can differ more. That is not a quality failure; it is what growing a material means.
The practical consequence is that you cannot specify a single visual standard. Instead you specify a range, and you document it with physical reference pieces rather than with adjectives. Ask for a submission of five to eight sheets from the batch you intend to buy, photograph them under consistent light, and agree which end of the range is acceptable and which is not.
Yield is the second honest constraint. Because sheets are smaller and irregular, nesting efficiency on a carrier pattern is typically lower than for a synthetic roll, and irregular edges increase waste. Build the yield assumption into your costing at a conservative figure and let the production team improve on it, rather than assuming best case and discovering the shortfall when the bulk is cut.
There is a design response to all of this, and it is more useful than any specification. Break the visible surface into multiple smaller panels rather than one large one. Smaller panels make variation read as intentional, raise yield, and give you natural places to introduce a contrast binding or a piping line. A carrier built from five mycelium panels looks deliberate; the same area in one panel looks like a material that could not be controlled.
The last constraint is time. Grow capacity is limited industry-wide, and a supplier's allocation is often booked months ahead. If a seasonal drop depends on mycelium, the reservation conversation happens before the design is final, not after. Build the material allocation into the critical path on the same footing as tooling or fabric booking, and name a fallback material early. A program with a pre-agreed substitute can absorb a supply surprise without losing the season; one without it usually loses both.
Branding a Mycelium Surface: What Holds and What Bleeds
The surface of a grown sheet is porous and slightly fibrous, which changes the branding toolkit in ways that are easy to underestimate. Methods that rely on a non-porous film behave differently here, and the usual sample-to-production gap is wider than on synthetics.
- Laser marking and engraving. The standout option. Mycelium responds to laser with a clean colour shift and a crisp edge, and the mark is permanent without adding any material. It also reinforces the material story in photography.
- Emboss and heat stamp. Reliable, and the compressible mat holds a pressed mark well. Keep deboss depth moderate; a deep press can thin the sheet enough to weaken it.
- Screen print. Feasible but variable. Ink sits differently on a fibrous face depending on local density, so expect a slightly organic edge. That can look intentional, or it can look like a reject.
- Woven label, rubber patch and metal badge. The safe choices when the brand mark has fine detail, and the ones I would recommend for a first program.
Two methods to avoid: dye sublimation, which needs a thermoplastic surface and the temperatures that come with it, and high-frequency welding, which needs a film the material does not have. If either is proposed, the conversation is about whether the supplier has run this material before.
Placement deserves the same three-position prototyping I would recommend on cork. Because density varies across a sheet, a laser mark can burn lighter or darker depending on where it lands. Test the mark at three positions on real sheets from the actual batch, and set the laser parameters from the densest area rather than the average, so the lightest result is still legible. Registration is the related risk: on a material that moves slightly during pressing, a mark placed close to a seam can drift by a millimetre or two. Keep branding at least 20 mm clear of any seam or binding so that drift reads as placement tolerance rather than as a misprint.
Colour and Finish When There Is No Dye Bath to Control
Mycelium sheets are usually coloured during growth or during finishing, not in a conventional dye bath, and that has a direct effect on what you can promise a brand team. Controlled, repeatable brand colour is the hardest thing to achieve in this category.
The realistic approach mirrors the one used for other natural substrates: accept a narrow family of earthy tones and express brand colour elsewhere. Mycelium naturally lands in a warm range from pale oat through tan to a deep brown, and within that range a supplier can usually hit a target with a stated tolerance. Outside it, particularly into cool or high-chroma territory, results become unpredictable and expensive.
Where precise colour matters, put it on elements you can control. Webbing, zipper tape, lining, printed labels and hardware can all be matched to a Pantone reference with a defined Delta E tolerance, and those elements carry brand recognition just as effectively as the body fabric. This is not a compromise; it is how most successful bio-material products are actually designed.
Finish choice then determines both appearance and serviceability. A minimal finish preserves breathability and the raw, tactile character, and it is the right choice for a product marketed on material honesty. A protective top-coat improves stain resistance and cleanability at the cost of some of that character and, usually, some of the claim. Decide which matters more for your customer before you ask for samples, because switching later means re-testing everything. A useful compromise is a differentiated finish: a light protective coat on the exterior panels only, with the interior left raw so the tactile character is still the first thing a customer feels when they open the carrier.
Pattern Design: Letting the Grown Panel Do What It Does Well
A mycelium panel is not a structural component. It has respectable tensile strength and poor tear resistance, it creeps under sustained load, and it dislikes tight folds. The pattern should reflect that from the first sketch rather than being corrected in the third sample round.
Start with a minimum bend radius. For a 1.5 mm sheet, keep internal folds at 12 mm or greater and bind anything tighter. Use generous seam allowance, around 15 mm, and a longer stitch length with a ballpoint needle so you are not perforating the mat along the seam line. Where a seam will carry load, add a woven reinforcement tape on the inside rather than relying on the sheet itself.
Second, decide where the material goes. The strongest architecture is the same hybrid that works for cork and apple leather: mycelium on the exterior face panels and lid, a proven coated woven on the base and gusset, and an internal frame or board carrying the shape. That keeps the grown material where customers see and touch it and keeps structural work on materials with a decade of field data.
Third, plan the edges. Raw mycelium edges are friable and will shed. Bind them, turn and topstitch them, or cover them with a webbing trim. The third option gives you a second colour placement and solves the durability problem at the same time.
Finally, remember breathability is a genuine advantage here. Unlike a coated synthetic, an unfinished mycelium panel moves air. If your carrier design has ventilation panels, placing the mycelium next to a mesh gusset lets you make an airflow argument that would be false on PU. Airline-compliant carriers are judged on ventilation as much as on dimensions, so this is a functional advantage rather than a marketing one, and it belongs in the product copy with the reasoning attached.
Cost, Scale and the Small-Batch Reality
Mycelium is currently a premium material by any measure, and it should be costed as one. Compared with a standard PU at a baseline of 1.0x, expect mycelium to land several multiples higher per square metre, with the multiple narrowing as grow capacity expands and widening for small or custom-finished lots.
| Cost lever | Effect | Trade-off |
|---|---|---|
| Panel zoning | Largest single saving | Base and gusset move to coated woven |
| Smaller panel layout | Raises nesting yield | More seams, more design lines |
| Stock finish instead of custom | Removes make-ready cost | Less exclusivity |
| Single colourway drop | Clears MOQ 500 cleanly | Narrower range in season one |
| Longer reservation lead time | Better allocation pricing | Less flexibility on launch date |
Scale is the harder constraint. Grow capacity is finite and demand from fashion and automotive is competing for it, so a brand planning a large program may find allocation rather than price is the binding limitation. For most carrier brands this argues for exactly the opposite of a broad rollout: a small, well-marketed drop in a single colourway, with the material positioned as the reason the run is limited.
That framing turns a supply constraint into a marketing asset. A 500-piece mycelium drop with a numbered hang tag is commercially stronger than a 5,000-piece rollout that strains the supply chain and dilutes the story. It also matches the material's actual availability, which is the most underrated form of launch planning. Pricing should reflect the same logic: cost the drop on the assumption that the entire run sells, and resist the temptation to amortise tooling across a hypothetical second season that capacity may not support. If the drop works, the second one will be easier to fund and easier to source, and the brand will have learned what customers actually think of the material before committing to volume.
Compliance, Certification and Novelty-Material Risk
Novelty materials attract two kinds of scrutiny: the chemical kind that every consumer product faces, and the claim kind that only new materials attract. Prepare for both.
On the chemical side, the requirements are unchanged. REACH SVHC declarations for the EU, a Prop 65 assessment for California, and an OEKO-TEX certificate on the finishing chemistry and any backing cloth are the baseline set. Because mycelium is grown on an agricultural substrate, it is worth asking specifically about pesticide residues and heavy metals in the feedstock; a serious supplier will have that data.
On the claim side, precision is your protection. "Grown from mycelium" is accurate. "Mushroom leather" is accepted shorthand in the trade and is how most buyers search for the category. "Plastic-free" is usually false, because most commercial sheets contain a binder and often a finish. "Home compostable" may be true for an unfinished sheet and is almost never true for a finished carrier with hardware, lining and webbing attached.
Traceability documentation is worth specifying at the outset. Ask for a batch record that ties the substrate, the grow parameters and the finish chemistry to the sheets you received. Independent verification adds credibility with retail partners; SGS testing and verification is the name most buyers recognise on a first submission.
Finally, extend the inspection standard. A generic bag checklist will not catch the failures this material produces, so write the AQL 2.5 defect list yourself and include surface voids, density variation beyond the approved range, edge friability, and finish inconsistency between panels.
Launch Strategy: Capsule, Waitlist and the Numbered Drop
Mycelium rewards a launch structure built around scarcity and punishes one built around breadth. The material's cost, availability and variability all point to the same plan: a single colourway, a fixed quantity, and a date.
A workable sequence starts with a reservation, made before the pattern is frozen, so the grow batch is secured. Then a three-round sample programme: material submission first, branding tests second, sewn prototype third. Sampling runs 6-10 working days once grade and finish are confirmed, bulk lands 35-50 days after approval, and a limited drop should add contingency for the possibility that the first batch does not match the reference set.
The product itself should carry the story physically. A numbered hang tag, a small insert explaining the two-to-four-week growth cycle, and a laser-marked batch code on the panel all cost very little and do more for perceived value than any amount of copy on a product page. Because the material looks unusual, customers want an explanation; give them one they can hold.
Packaging should be consistent with the claim. A rigid box is defensible at this price point, but it should be a recycled or recycled-content board, because a virgin-board luxury box around a grown-material product invites an obvious question the customer will ask themselves.
Plan the follow-up while the first drop is still running. If it sells through, the reorder conversation is about a new grow batch, which means new reference samples and a documented tolerance rather than an exact match. Say so on the product page from the start and the second drop becomes evidence of authenticity rather than a quality complaint. Keep the batch code on the hang tag through every subsequent run, so a customer who owns drop one can see the lineage rather than assuming the brand changed supplier.
Why brands source here
- Pet carrier programs run since 2014; founding team in sewn goods since 2004
- SGS-verified production floor of 4,950 m² with 137 workers across 7 lines
- Monthly capacity of 200,000 units, audited to BSCI and ISO 9001
People Also Ask
What is mycelium leather?
Mycelium leather is a material grown from the root network of a fungus on an agricultural substrate. The resulting mat is dried and pressed into a sheet that is used as a leather substitute in bags, footwear and accessories.
Is mushroom leather the same as vegan leather?
It is one type of vegan leather. The broader category also includes PU, cork, apple, pineapple and cactus materials, each with a very different performance and cost profile.
How strong is mycelium leather?
Tensile strength typically falls between 4 and 12 MPa depending on density and growth time. Tear strength is the more useful figure for a sewn product and is the number a brand should insist on.
Why is mushroom leather expensive?
Grow capacity is limited, cycle times are measured in weeks, and finishing is labour intensive. Price is expected to fall as capacity scales, but it remains a premium material today.
Does mushroom leather smell like mushrooms?
A finished sheet has a faint earthy note when new that dissipates quickly. It is much less pronounced than the odour of a low-grade PVC coating and is rarely noticed by customers.
Can mushroom leather be embossed?
Yes. The mat compresses cleanly under a heated die and holds the impression. Keep deboss depth moderate, since a deep press thins the sheet and can weaken the panel.
Frequently Asked Questions
Is mushroom leather durable enough for a pet carrier?
For exterior panel use, yes, with reinforcement. Specify a grade with tear strength of at least 25 N and move the base, gusset and interior load paths to a proven coated woven so the grown panel never carries structural work.
What is mushroom leather actually made of?
It is grown from mycelium, the root network of a fungus, fed on an agricultural substrate such as sawdust or hemp hurd. The colonised mat is dried, pressed and finished into a sheet. The fruiting body is not used.
How long does it take to grow a mycelium sheet?
Typically two to four weeks of growth, followed by drying, pressing and finishing. The growth time sets the density of the mat and therefore the hand and strength of the finished sheet.
Can mycelium leather be matched to a brand Pantone colour?
Within its natural warm range, yes, with a stated tolerance. Outside that range results become unpredictable. Precise brand colour is better carried by webbing, lining, zipper tape and hardware, which can be matched exactly.
Does mushroom leather absorb water?
An unfinished sheet does absorb moisture and will stain. A protective top-coat largely solves this at the cost of some of the raw character. Either way, a carrier should still specify a liner in the interior.
What is the MOQ for a mycelium carrier drop?
MOQ is 500 pieces per colourway. Given grow capacity constraints, a single-colourway drop of 500 units is usually a stronger commercial plan than a larger multi-colour program.
Can you laser engrave a logo onto mycelium leather?
Yes, and it is the best branding method available on this material. The laser produces a clean, permanent colour shift with a crisp edge and no added material, which suits the material story well.
Will two mycelium panels look the same?
No. Density, texture and shade vary within and between grow batches. Manage this with a physical reference set agreed before bulk rather than with a written description, and design with multiple smaller panels so variation reads as intentional.
Is mushroom leather vegan and plastic-free?
It is vegan, containing no animal input. It is not usually plastic-free, because most commercial sheets use a binder and often a synthetic finish. State the composition you can document.
Is mushroom leather compostable?
An unfinished sheet may be, but a finished carrier with hardware, lining, webbing and a top-coat is not. Do not market the assembled product as compostable.
How does mycelium compare with cork and apple leather?
It is the softest and most irregular of the three, and the most expensive. Cork is lighter and more abrasion resistant; apple leather is the most consistent and the easiest to brand. Mycelium wins on distinctiveness.
What inspection level applies to a mycelium production run?
Inspection runs at AQL 2.5 against a signed golden sample, with a defect list extended to include surface voids, density variation outside the approved range, edge friability and finish inconsistency.
How long does a mycelium carrier program take?
Sampling takes 6-10 working days once grade and finish are fixed, and bulk runs 35-50 days after approval. Secure the grow batch reservation before the pattern is frozen, and hold contingency for a first batch that misses the reference range.
Talk to QUANZHOU JUNYUAN BAGS about a pet carrier program: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production in 35-50 days under AQL 2.5 inspection.
Get a free quote Request a sample